From SMT line to burn-in — inside the factory
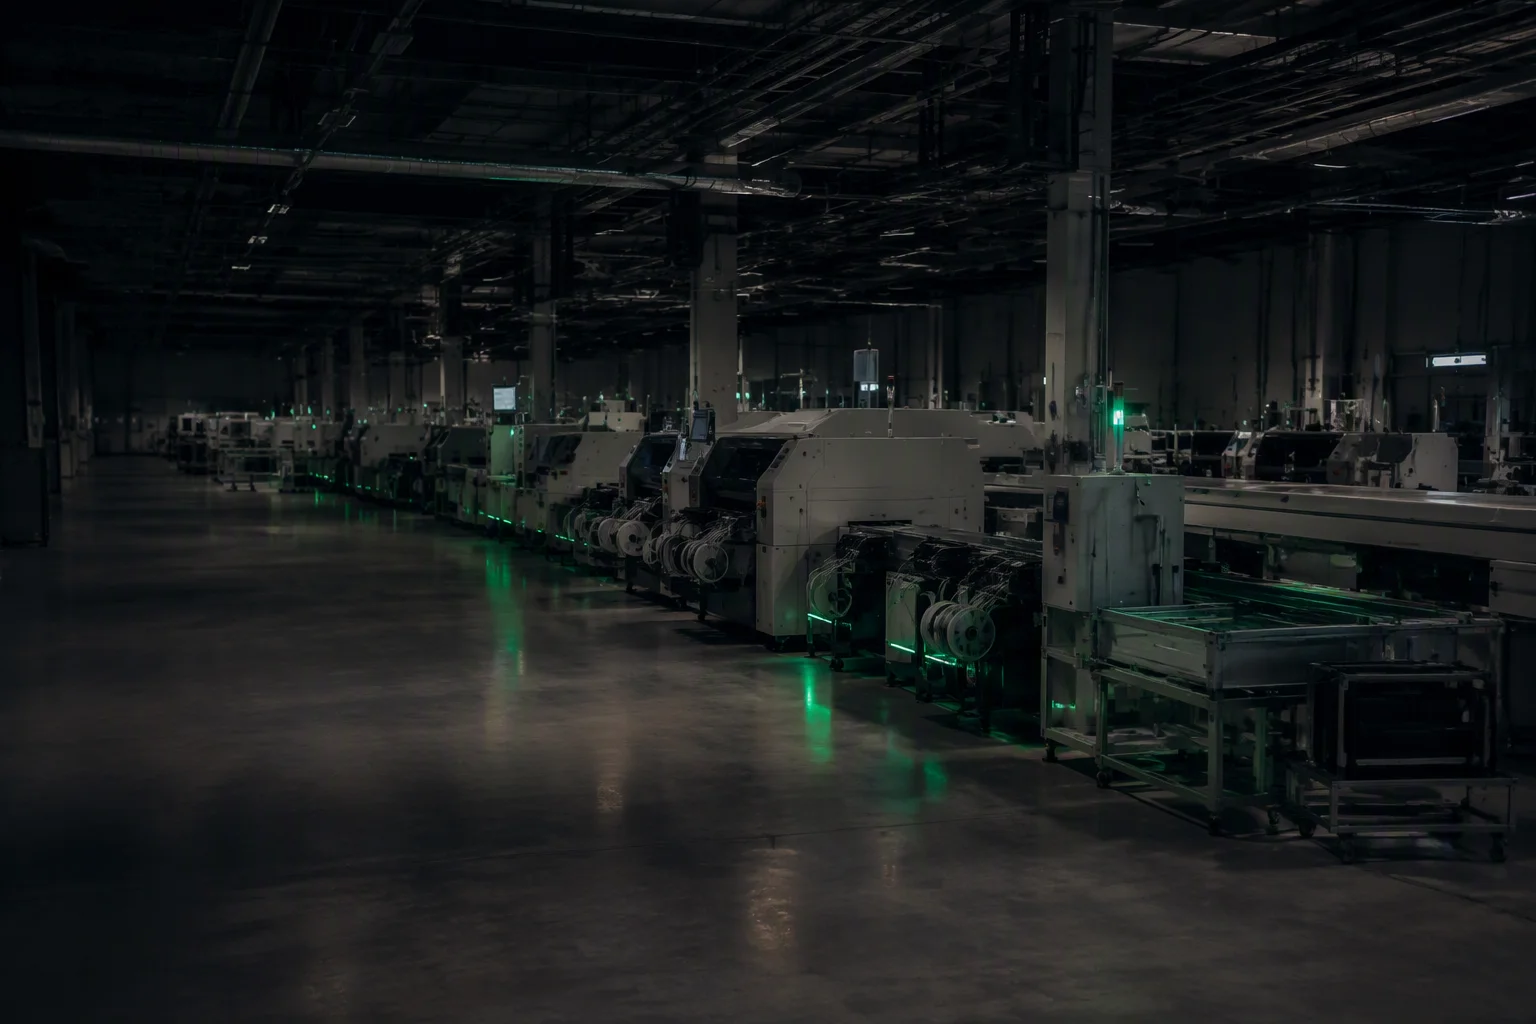
A 20,000 m² Shenzhen facility where every charger is built on an automated SMT line, assembled from in-house power modules, and finished with 48 hours of burn-in and 33 environmental tests before it ships.
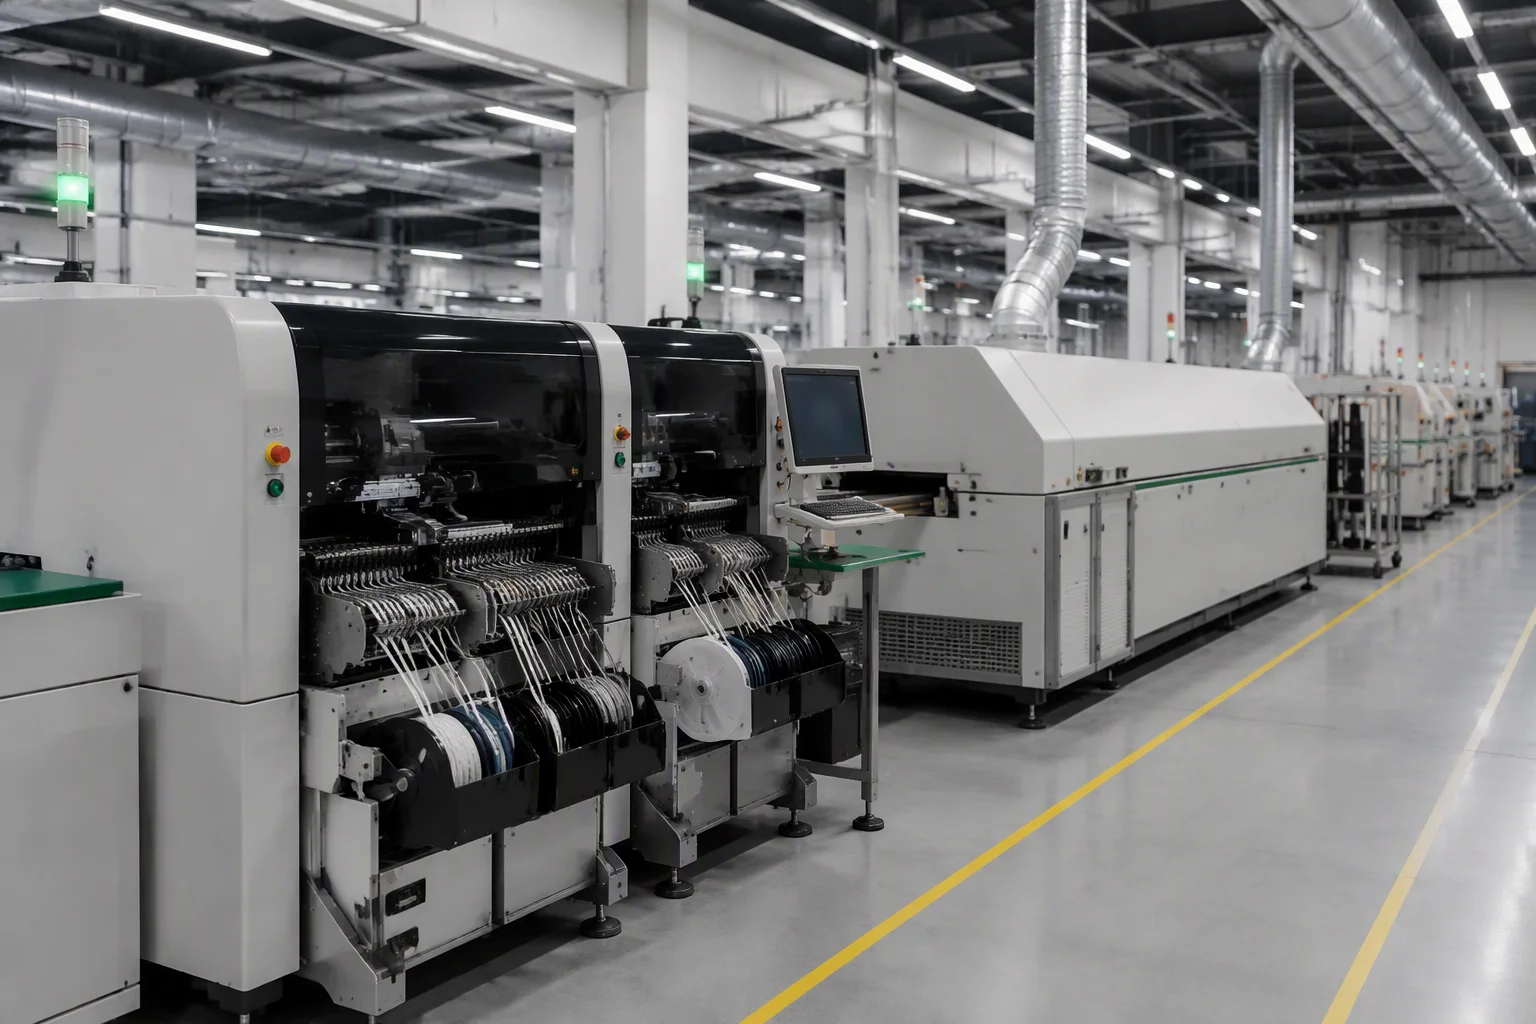
Automated from board to cabinet.
Six SMT lines place surface-mount components for control, metering and communication boards, then feed module assembly and final integration. We hold the process in-house so a firmware change and a hardware change land on the same line.
- SiC power electronics lift system efficiency 5–10% and cut cooling volume 30–40% versus IGBT designs.
- Vienna rectifier + LLC resonant topology keeps input current harmonics (THDi) under 5%.
- 48-hour burn-in at elevated ambient on every DC unit before the environmental chamber.
- 20,000 m² of SMT, module, assembly, test and warehouse space under one roof.
The machines behind the modules.
Every stage is instrumented — placement, solder profile, full-load calibration and environmental stress are measured, not assumed.
| Equipment | Process | What it verifies |
|---|---|---|
| SMT pick-and-place | PCB assembly | 0201–01005 components, ±0.02 mm placement |
| Reflow oven | Soldering | 10-zone profile, nitrogen option |
| Wave soldering | Through-hole | High-current board joints |
| AOI inspection | PCB QC | Post-solder optical verification |
| Conformal coating | Protection | IP-rated board coating |
| Module test bench | Power modules | 30/40 kW full-load calibration |
| Burn-in chamber | Aging | 48 h at elevated ambient |
| Temperature chamber | Environmental | −35°C to +55°C cycling |
| EMC anechoic chamber | Emissions | CISPR 11/32 Class B |
| IP rain test rig | Ingress | IPX5/IPX6 water jets |
| Salt-spray chamber | Corrosion | 96-hour neutral salt fog |
| Power analyzer | Efficiency | 0.05% load measurement |
Six stages, one accountable line.
SMT
Control, metering and comms boards are placed and reflow-soldered on automated lines with AOI after reflow.
Power modules
SiC and IGBT stages are built on the Vienna + LLC topology and calibrated to full load on the bench.
Assembly
Cabinets, cooling, cabling and connectors are integrated, then the unit is flashed and configured.
Burn-in
48 hours of powered aging at elevated ambient catches infant failures before they leave the factory.
Environmental
33 thermal, EMC, rain and salt-fog tests across −35°C to +55°C prove the enclosure and electronics.
PSI
A pre-shipment inspection report with photos and test data ships with the packing list.
Capacity that scales with your order.
Tested harder than it will be used.
The charger is designed to run at −30°C to +55°C, so we qualify it beyond that envelope and against the standards your market enforces.
33 environmental tests
Thermal shock and cycling from −35°C to +55°C across every SKU, not a sample.
EMC & harmonics
CISPR 11/32 Class B emissions and THDi under 5% verified in the anechoic chamber.
Ingress & corrosion
IPX5/IPX6 water jets and 96-hour salt fog confirm IP54/IP65 enclosures hold.
See the line, or start a build.
Book a video factory tour, or send your spec — we return specs, pricing and lead time within 48 hours.
Send Inquiry